The 5 PLC Programming Languages and When to Use Each
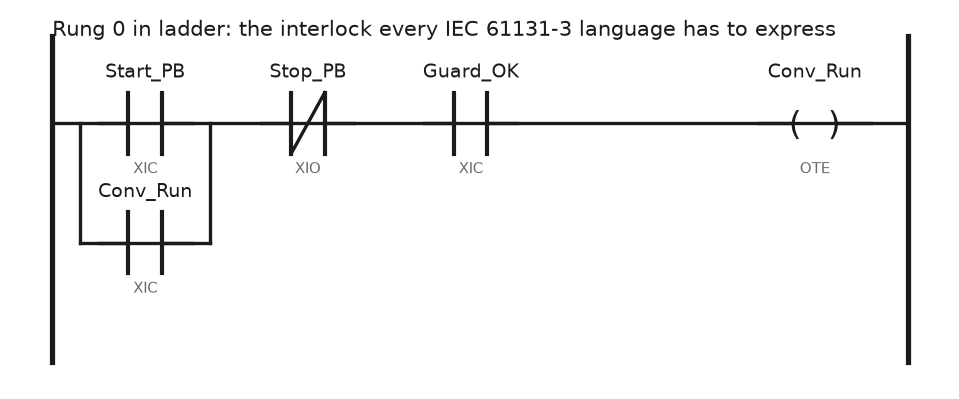
Ladder, FBD, Structured Text, SFC and IL compared on real hardware: what Studio 5000 v33 and TIA Portal V18 support, and which one to pick per job.
Ladder, FBD, Structured Text, SFC and IL compared on real hardware: what Studio 5000 v33 and TIA Portal V18 support, and which one to pick per job.
A TON with a .PRE of 5000 that sits in a subroutine only called in Auto, with its rung left true, is already done on the first scan back after twenty minutes in Manual. Publication 1756-RM018A-EN-P prints the arithmetic that explains it, ACC = ACC + (current_time – last_time_scanned), so the timer bills the whole … Read more
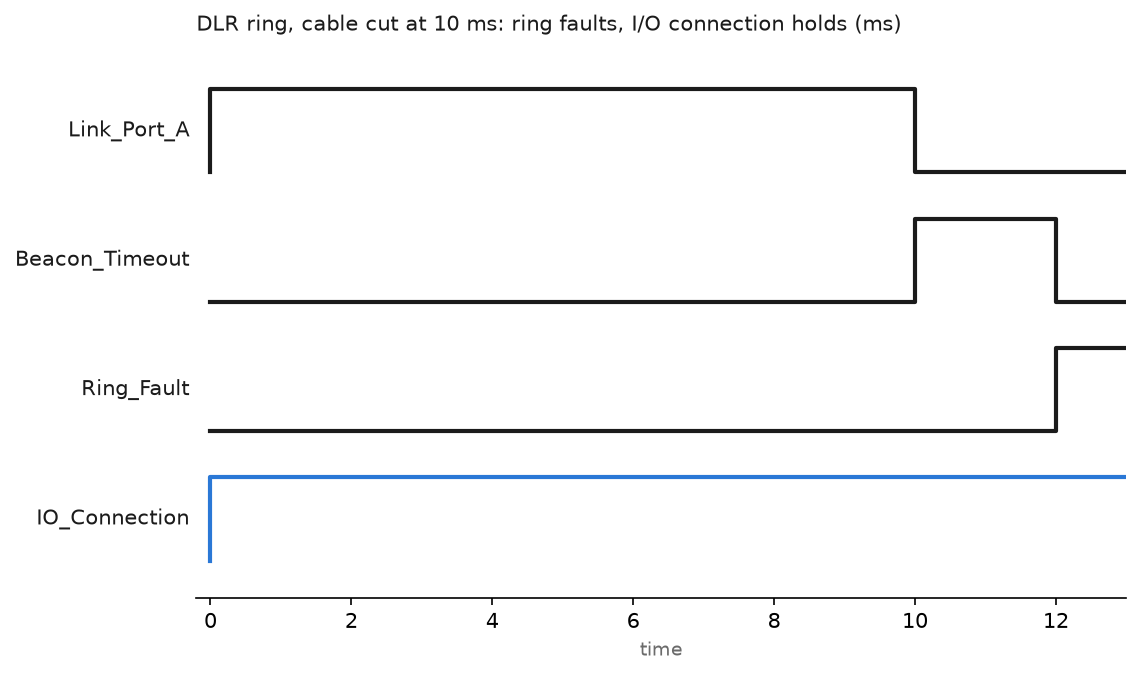
PLC networking done properly: switch features that matter, an address plan, VLANs, DLR rings with 1783-ETAP, PROFINET RT and IRT, NAT and port numbers.
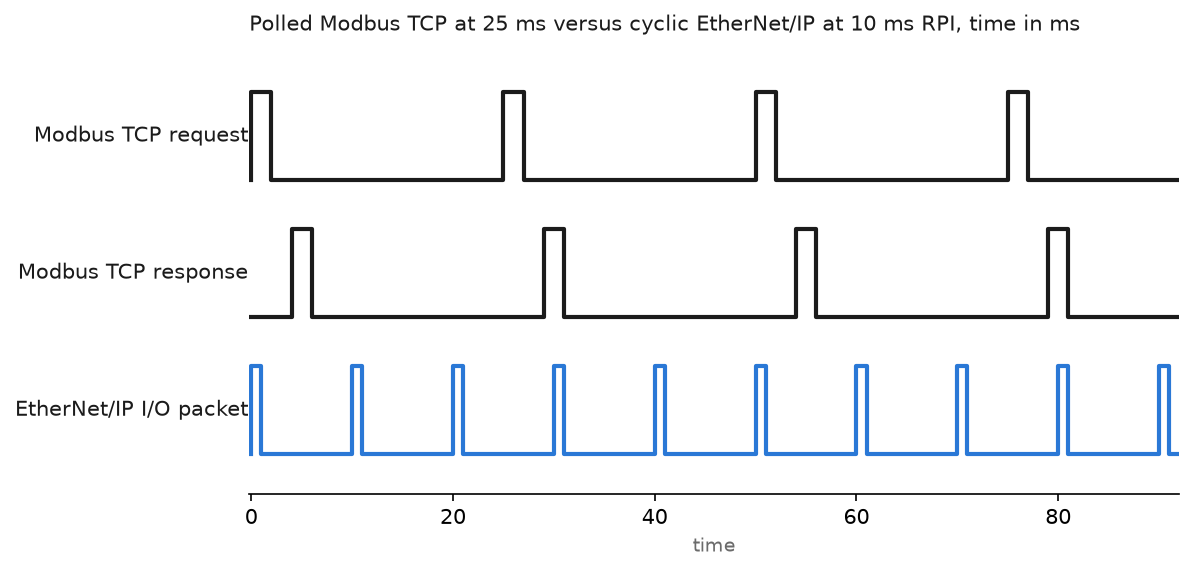
Modbus TCP, EtherNet/IP, PROFINET, OPC UA and MQTT compared by how they move data, with ports, poll rates and the mistakes that cost SCADA update time.
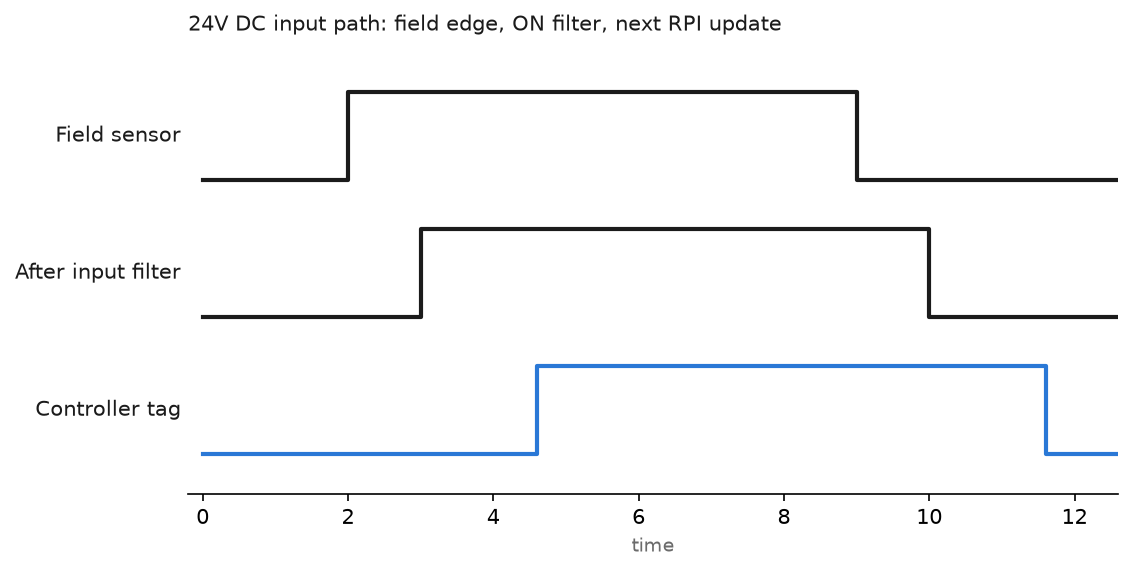
How to pick discrete and analog I/O, get sinking and sourcing right, set RPI and electronic keying, wire a 4-20 mA loop and scale the raw counts.
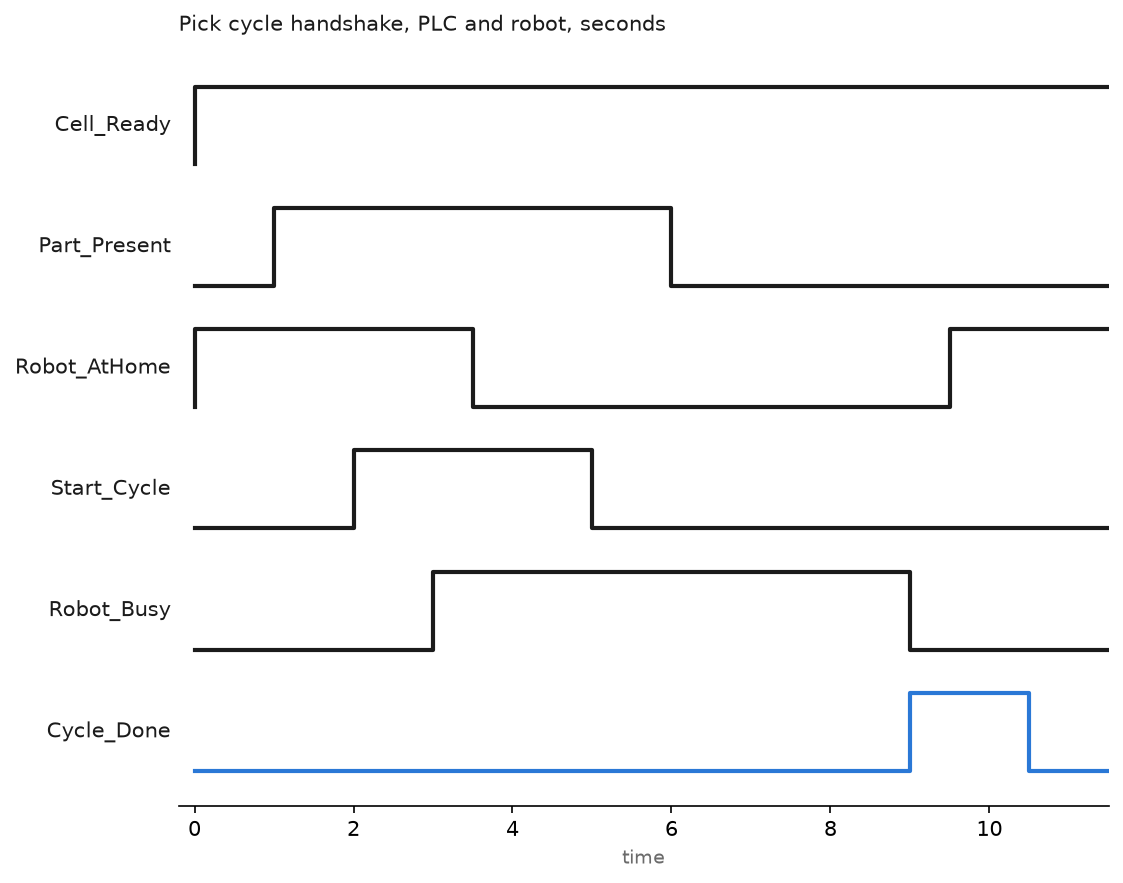
Map FANUC, ABB and KUKA signals into a PLC, build a pick cycle handshake that cannot drop, select the program by number, and set a sane RPI.
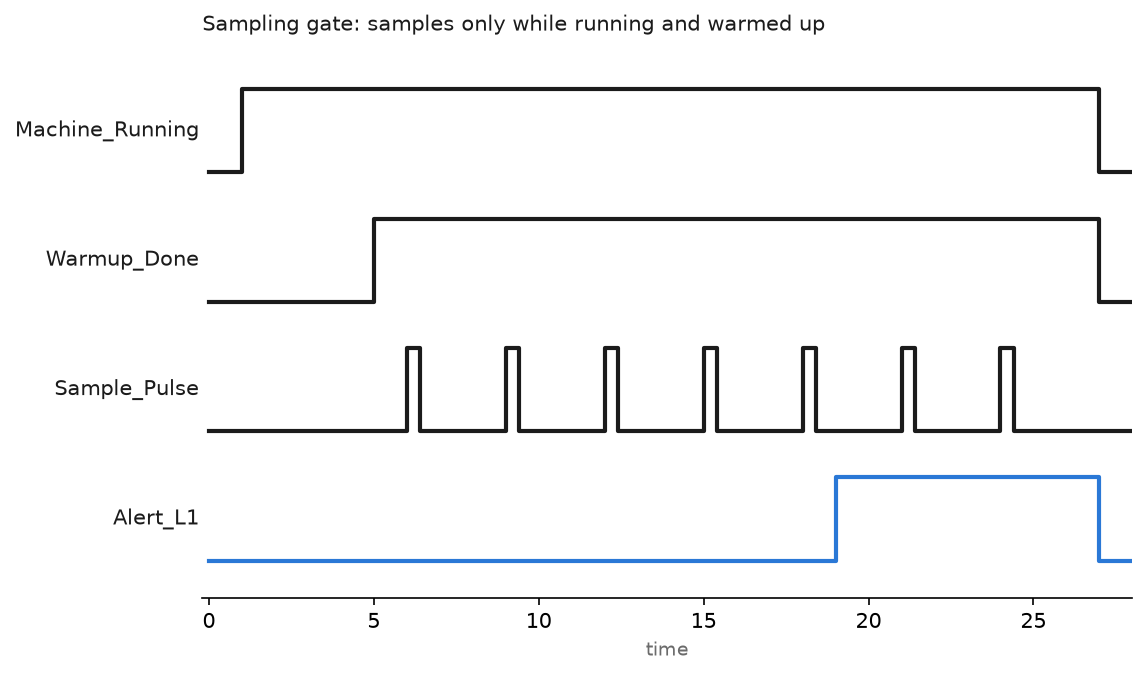
Build PLC predictive maintenance on hardware you own: vibration and motor current inputs, runtime hours, moving averages, baselines and alarm levels.
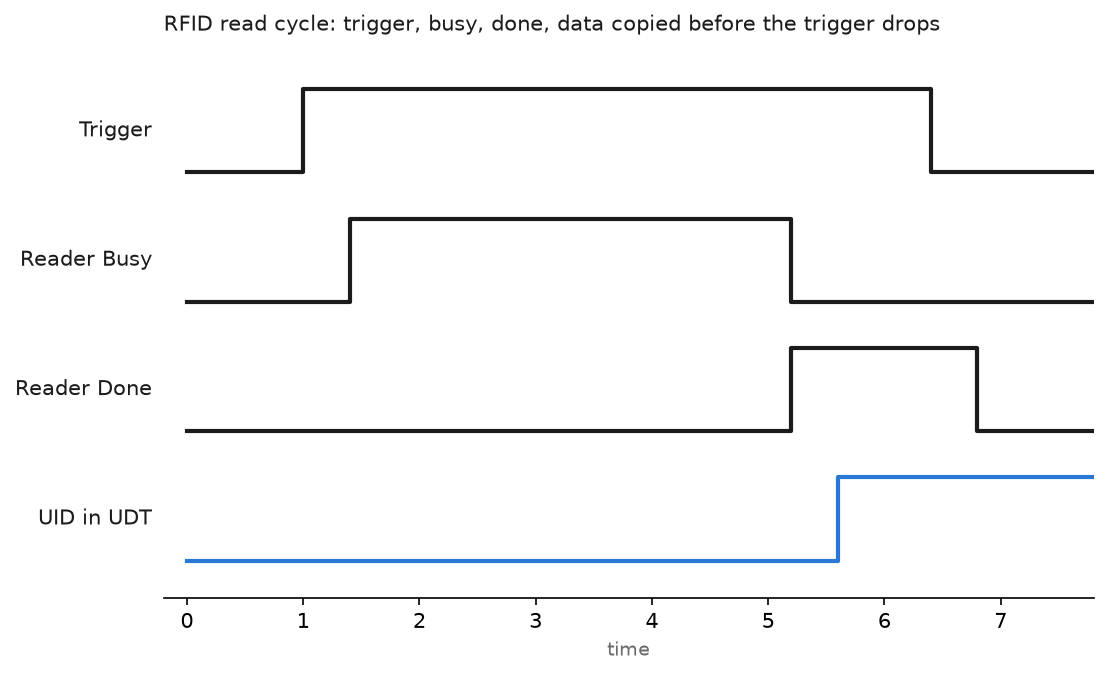
Pick HF or UHF, connect the reader over EtherNet/IP or Modbus, map the data into a UDT, and run a trigger, busy, done handshake that does not drop reads.
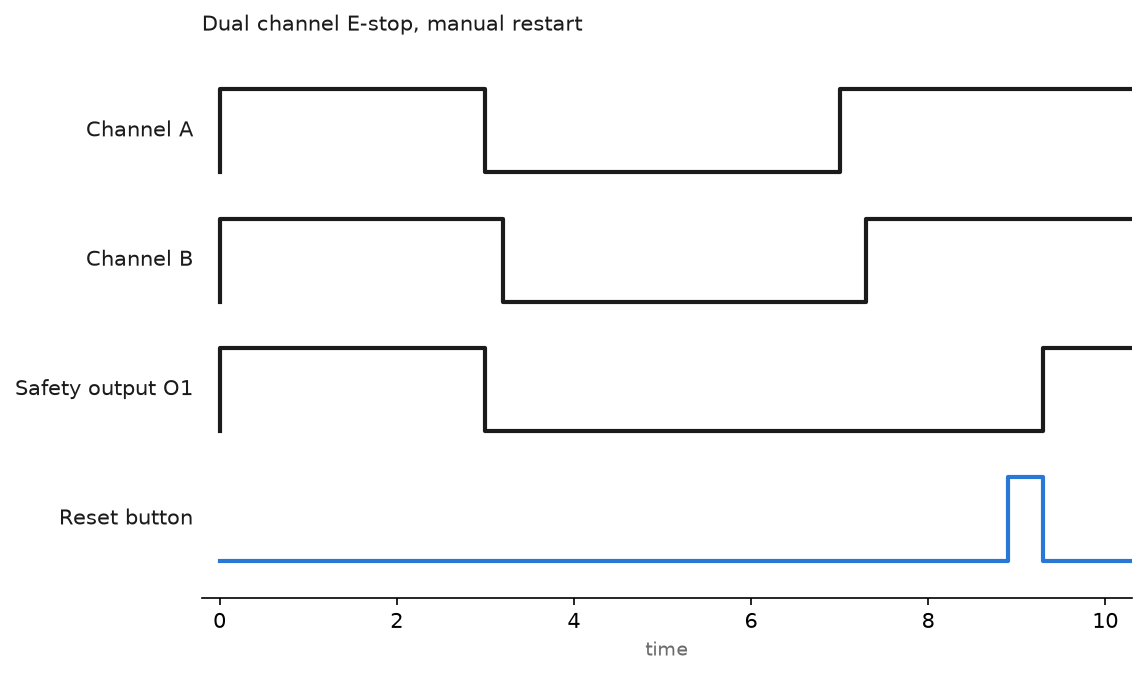
When a standard interlock is not enough, how to wire and configure a dual-channel E-stop on GuardLogix safety I/O, and the reset rule nobody may break.
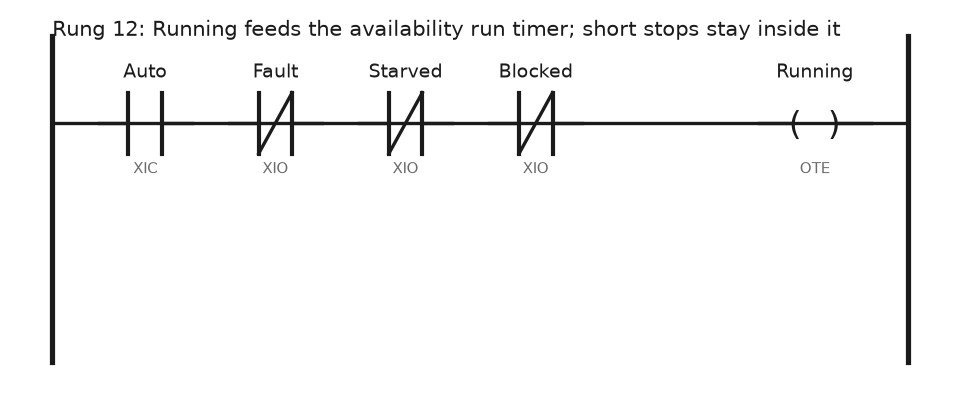
How a PLC state model feeds OEE, downtime reason codes and SPC triggers on a rotary filler: the ST block, the tag structure and the classic mistakes.
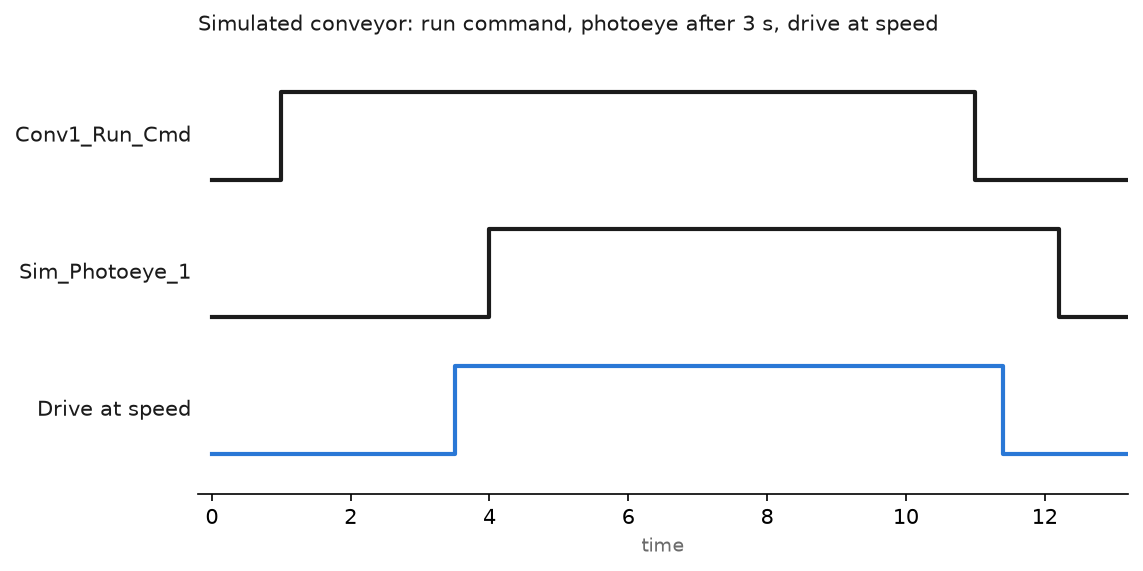
Build a Logix Emulate chassis, run PLCSIM Advanced, test the HMI offline, and learn which parts of a machine you can trust a simulation to prove.
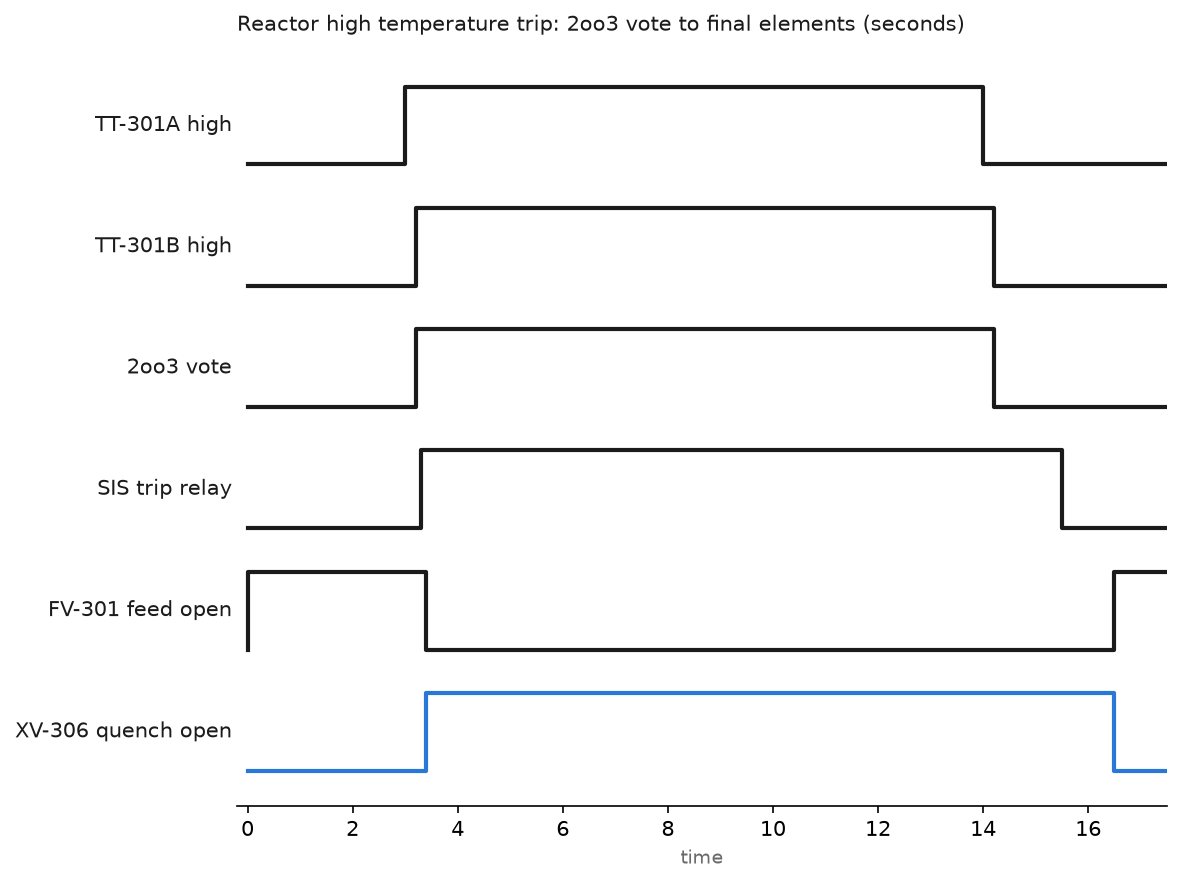
How the BPCS, the SIS and the package PLC split the work on a batch reactor, with a cause and effect matrix, cascade temperature control and IS barriers.